Top China Pharmaceutical Dust Collector Manufacturers for Your Factory Needs
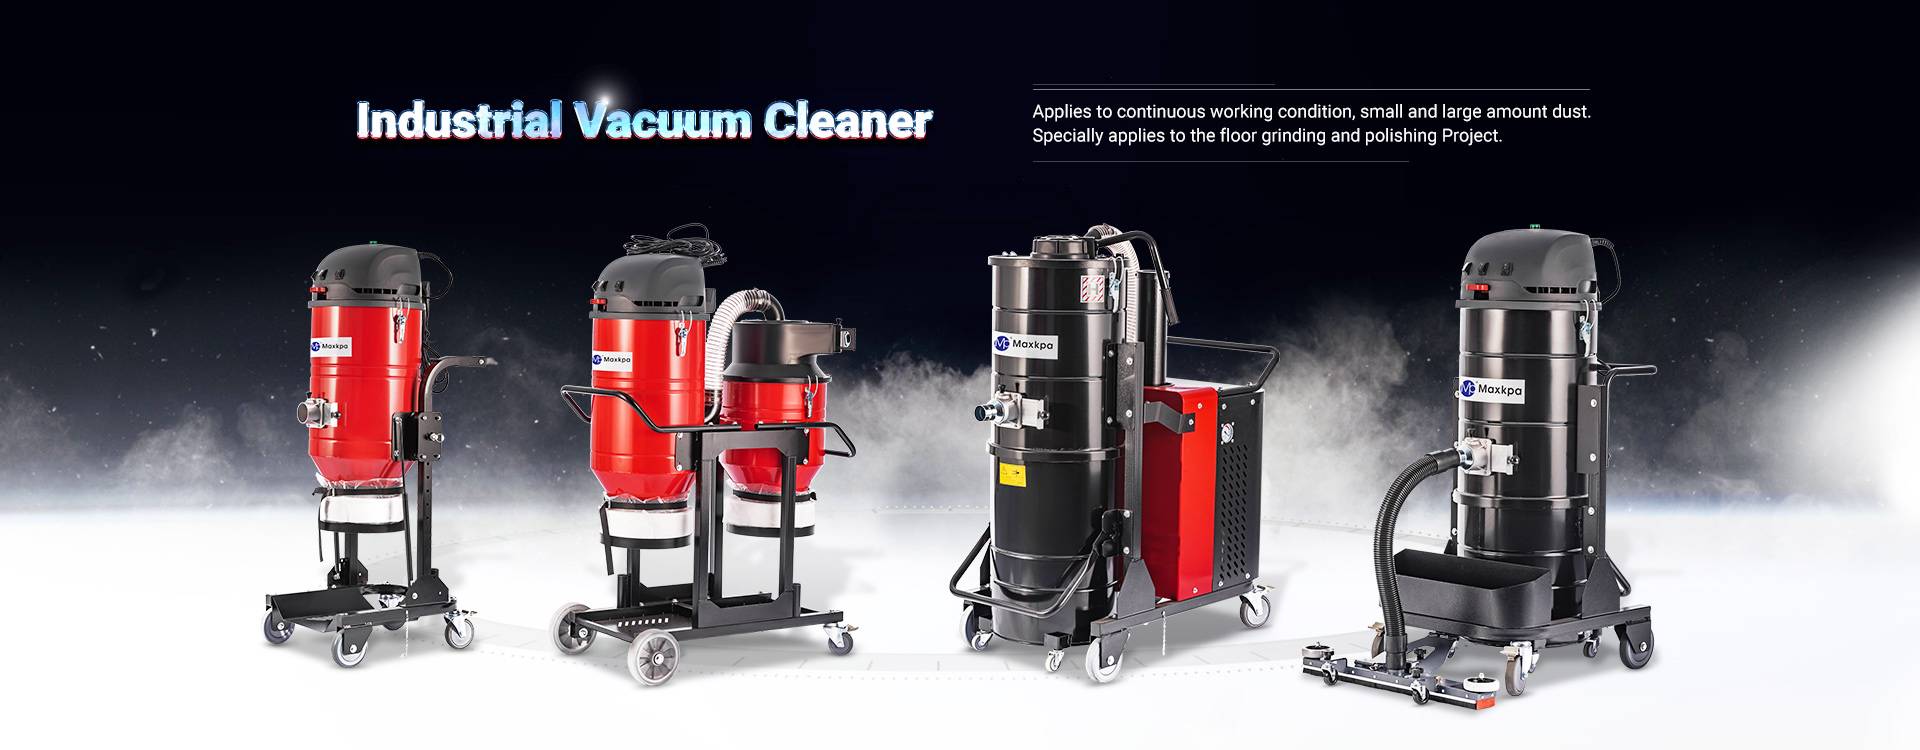
When I think of efficient solutions for capturing harmful powders in a pharmaceutical setting, the importance of a top-notch Pharmaceutical Dust Collector cannot be overstated. As a key factor in ensuring worker safety and compliance, this equipment stands out, particularly from reputable manufacturers in China. Our factories specialize in crafting state-of-the-art dust collection systems tailored for the pharmaceutical industry. We understand the unique challenges your business faces, and we put in the effort to deliver robust, reliable, and effective dust collection solutions that meet stringent regulatory standards. With our products, you’ll not only protect your workforce but also enhance your operational efficiency. As a partner in your success, I’m excited to help you navigate the myriad of options available, ensuring you find the perfect dust collector that aligns with your specific needs. Invest in a cleaner, safer workplace with our expertly-designed solutions that’ll elevate your production standards.
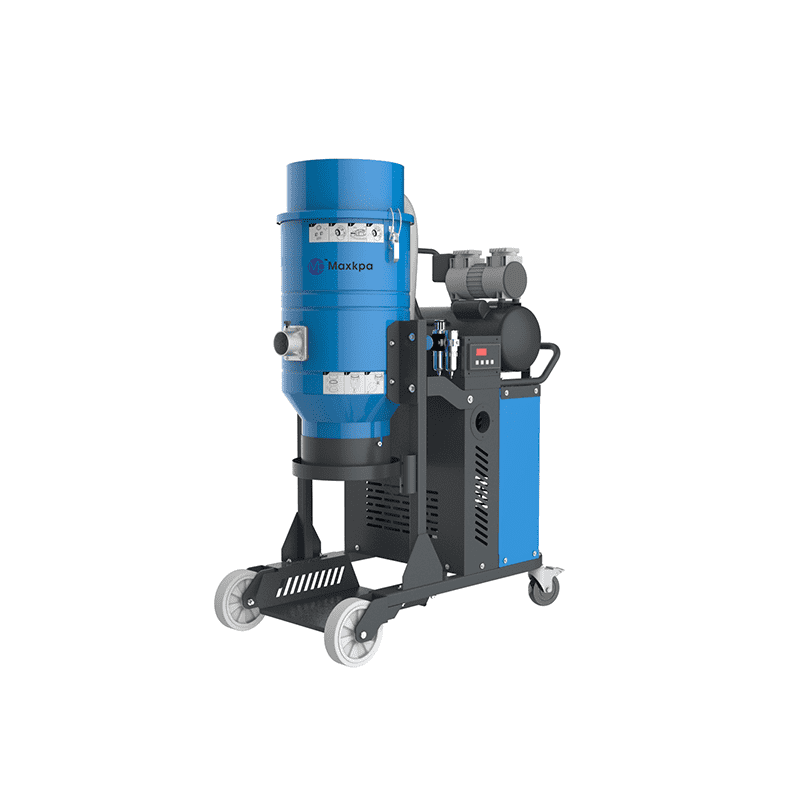
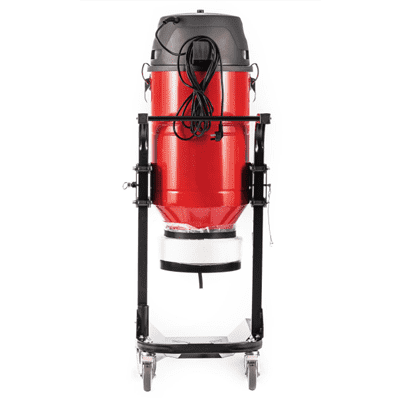
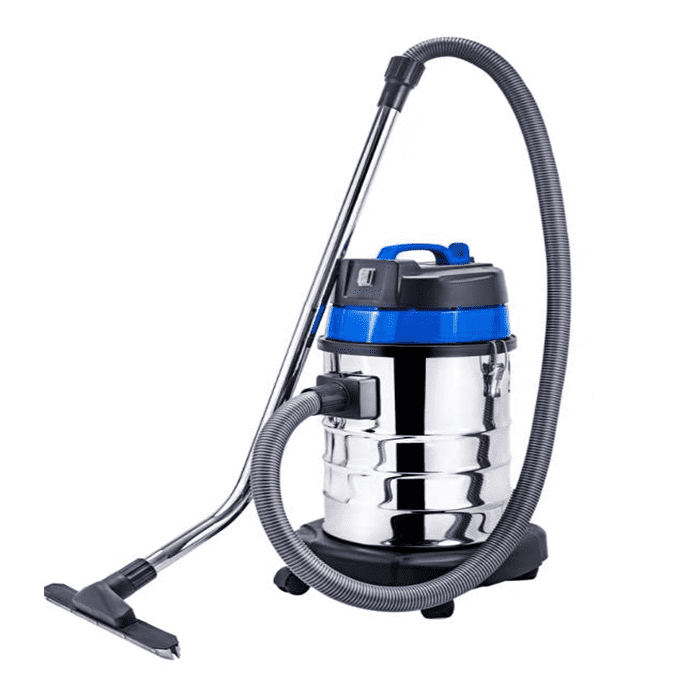
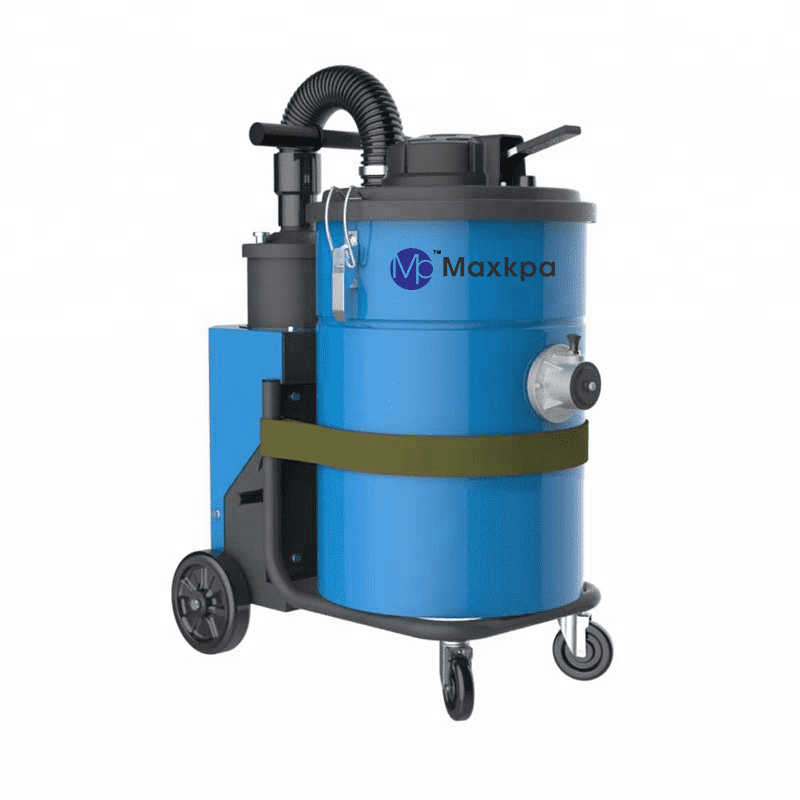
Pharmaceutical Dust Collector Factories Factory Is The Best
When sourcing pharmaceutical dust collectors, it's essential for global buyers to focus on manufacturers that deliver both quality and reliability. With the increasing demand for dust management solutions in the pharmaceutical industry, selecting a factory known for its innovative design and advanced technology becomes paramount. A top manufacturer ensures that their dust collectors meet stringent industry regulations while enhancing operational efficiency. Investing in a high-quality pharmaceutical dust collector not only improves workplace safety but also streamlines production processes. Features such as efficient filtration systems, low energy consumption, and minimal maintenance requirements make these machines a crucial asset for any pharmaceutical facility. Buyers should seek out manufacturers that prioritize research and development, as this commitment leads to improved product longevity and effectiveness in controlling airborne particles. Furthermore, a factory that offers customizable solutions can cater to specific operational needs, ensuring that the dust collector integrates seamlessly into existing workflows. The best manufacturers also provide robust customer support and after-sales service, assisting clients in optimizing their systems for maximum performance. By choosing a reputable supplier, global buyers can enhance their production capabilities while maintaining high standards of safety and compliance in the pharmaceutical sector.
Pharmaceutical Dust Collector Factories Factory Is The Best
| Factory Location | Production Capacity (kg/h) | Filtration Efficiency (%) | Certifications |
|---|---|---|---|
| City A | 500 | 99.9 | ISO 9001, CE |
| City B | 400 | 99.5 | ISO 14001, GMP |
| City C | 600 | 99.8 | ISO 45001, FDA |
| City D | 550 | 99.6 | ISO 9001, CE |
| City E | 700 | 99.7 | GMP, FDA |
Related Products


Pharmaceutical Dust Collector Factories Service From Concept to Delivery
Top Selling Products


- Related Blog
- Reviews
